Custom Plate Freezer Manufacturer: Innovative Solutions for Industrial Cooling
2026-04-16
In today's rapidly evolving industrial landscape, efficient cooling solutions are more critical than ever—especially for sectors requiring precision and scalability. Amidst a sea of options, one name stands out for transforming the way businesses approach frozen storage and processing: Worldbase. As a leading custom plate freezer manufacturer, Worldbase doesn't just produce equipment; it crafts bespoke, innovative solutions tailored to meet the unique demands of industrial cooling. From food processing to pharmaceuticals, their technology ensures optimal temperature control, energy efficiency, and reliability. But what truly sets Worldbase apart? In this blog, we'll dive into their cutting-edge approach, explore how custom plate freezers are revolutionizing industrial operations, and uncover why forward-thinking companies are turning to Worldbase for their cooling needs. Get ready to discover the future of industrial cooling—where innovation meets practicality.
Advancing Industrial Cooling with Custom Plate Freezers
The industrial sector is always on the lookout for smarter, more efficient ways to manage its cooling needs, and custom plate freezers are stepping up to the plate—quite literally. Unlike off-the-shelf models that might force a square peg into a round hole, these tailored solutions are designed from the ground up to fit specific production lines and product types. Imagine a seafood processing plant where irregularly shaped fillets or whole fish require uniform freezing to maintain quality and texture; a custom plate freezer can be engineered with varying plate sizes or adjustable pressure settings to ensure every piece gets the same precise treatment. This level of customization not only boosts efficiency by reducing energy waste but also minimizes product damage, leading to higher yields and better end results. It's about turning cooling from a generic step in the process into a finely tuned art form.
Beyond just fitting the physical dimensions, custom plate freezers excel at adapting to the unique thermal demands of different industries. In pharmaceuticals, for instance, strict temperature control is non-negotiable to preserve the integrity of sensitive compounds. A bespoke system might incorporate advanced sensors and automated controls that adjust cooling rates in real-time, ensuring consistency that standard units can't match. Or take the beverage industry, where rapid freezing of liquid concentrates is crucial to lock in flavor and extend shelf life; custom-designed plates with enhanced surface area can achieve faster freeze times without compromising on temperature stability. By addressing these niche challenges, custom plate freezers don't just keep things cold—they optimize the entire cooling cycle, making operations smoother and more reliable. It's a game-changer for businesses that can't afford one-size-fits-all solutions.
What really sets custom plate freezers apart in today's competitive landscape is their role in driving sustainability and long-term cost savings. While initial investment might be higher, the precision engineering involved often leads to lower energy consumption over time, as the system isn't overworking to compensate for poor fit. For example, a food manufacturer using a custom freezer might see reduced electricity bills thanks to better insulation and targeted cooling zones, alongside less downtime for maintenance because parts are built to last. Plus, with growing consumer and regulatory pressure for greener practices, these systems can be designed with eco-friendly refrigerants or recyclable materials, adding an extra layer of appeal. In essence, they're not just an upgrade in cooling technology—they're a strategic move toward more resilient, forward-thinking industrial operations that stand out from the crowd.
Key Design Features of Personalized Plate Freezer Systems
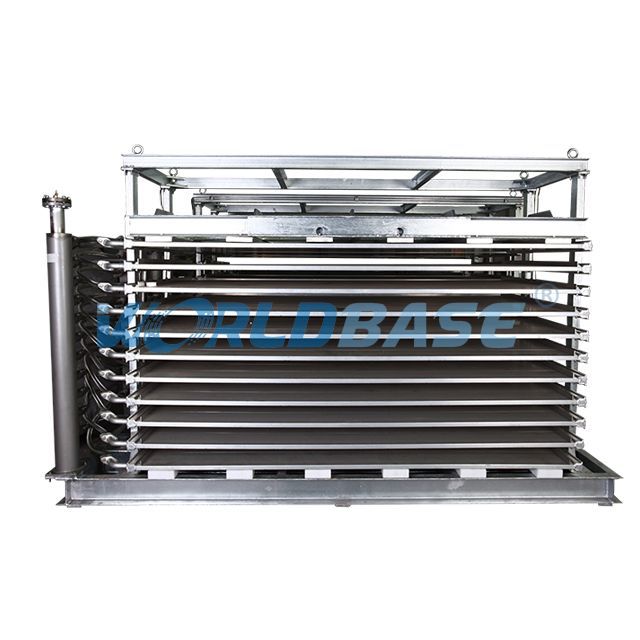
Personalized plate freezer systems are engineered with adaptability at their core, allowing for precise temperature control tailored to each product’s unique thermal properties. Unlike standard models, these systems incorporate modular plates that can be adjusted in spacing and pressure to accommodate varying thicknesses, from delicate seafood to dense meat portions, ensuring even freezing without compromising texture. Advanced sensors monitor real-time conditions, enabling operators to fine-tune cooling rates, which minimizes ice crystal formation and preserves flavor and nutritional content.
Another standout feature is the integration of user-friendly interfaces and automation technologies, which streamline operations in diverse settings like small-batch artisanal production or large-scale industrial facilities. By offering customizable programming for freeze cycles and defrosting protocols, these systems reduce manual intervention while boosting efficiency. This flexibility not only cuts energy costs but also supports rapid product changeovers, making them ideal for facilities handling multiple items with different freezing requirements.
Furthermore, these systems emphasize durability and hygiene through materials like corrosion-resistant stainless steel and seamless plate designs that simplify cleaning. Enhanced insulation minimizes thermal loss, contributing to sustainability goals by lowering overall energy consumption. Such attention to detail ensures reliable performance over time, helping businesses maintain high standards in food safety and quality while standing out in competitive markets.
Optimizing Frozen Product Quality through Custom Engineering
Ever noticed how some frozen foods just taste fresher and retain their texture better than others? That's not accidental—it's often the result of tailored engineering approaches designed specifically for each product type. While standard freezing methods might get the job done, they can sometimes lead to ice crystals forming inside the food, which damages cellular structures and results in a mushy or bland outcome upon thawing. Custom engineering steps in to address these nuances, allowing companies to fine-tune every aspect of the freezing process based on the product's unique composition, whether it's a delicate seafood item or a hearty vegetable mix.
What sets custom engineering apart is its ability to integrate advanced technologies like cryogenic freezing or controlled-rate freezing systems that adapt to the specific thermal properties of different foods. For instance, a flash-freezing technique might be employed for berries to lock in their juiciness and color, while a slower, more controlled process could be used for meats to prevent freezer burn and preserve tenderness. This isn't just about dropping temperatures; it's about creating a bespoke environment that minimizes quality loss, extends shelf life without relying on excessive preservatives, and ultimately delivers a product that feels almost as good as fresh.
Beyond the technical specs, custom engineering opens doors to innovation in product development, enabling brands to launch items that were previously too fragile for standard freezing. Think of gourmet meals with intricate layers or exotic fruits that travel long distances—these benefit immensely from processes tailored to their specific needs. By focusing on quality optimization through such personalized solutions, businesses not only enhance consumer satisfaction but also reduce waste and improve efficiency in their supply chains, making it a smart investment for both the palate and the planet.
Enhancing Production Efficiency with Tailored Freezer Solutions
In today's fast-paced manufacturing environments, every second counts, and customized freezer solutions are proving to be game-changers. By aligning freezer specifications precisely with production needs, companies eliminate unnecessary downtime caused by equipment mismatches. For instance, a food processing plant might integrate a modular blast freezer that adapts to varying batch sizes, streamlining cooling cycles without compromising quality.
Beyond just temperature control, tailored freezers incorporate smart features like energy-efficient compressors and automated defrost systems, which reduce operational costs significantly. This personalized approach not only boosts throughput but also minimizes waste, as products are frozen at optimal rates tailored to their specific characteristics, ensuring consistency and shelf-life extension.
Ultimately, investing in bespoke freezer technology fosters a more resilient production line, where flexibility meets reliability. Companies report smoother workflows and enhanced product integrity, translating into tangible gains in both efficiency and customer satisfaction.
Sustainable Practices in Customized Industrial Freezing Technologies
In the realm of industrial freezing, sustainability is no longer just a buzzword but a fundamental driver of innovation. Customized industrial freezing technologies are designed to meet specific operational needs while minimizing environmental impact. For instance, advanced systems incorporate energy-efficient compressors and eco-friendly refrigerants, such as those with low global warming potential, to reduce greenhouse gas emissions. These tailored solutions not only enhance product quality by preserving freshness and texture but also cut down on energy consumption, leading to significant cost savings over time.
Beyond energy efficiency, sustainable practices often involve optimizing resource use throughout the freezing process. Customized technologies enable precise control over freezing rates and temperatures, which can minimize water and cooling fluid waste. This precision helps prevent overfreezing or underfreezing, ensuring that raw materials are utilized efficiently without unnecessary spoilage. By integrating smart sensors and IoT devices, facilities can monitor and adjust conditions in real-time, further reducing waste and supporting circular economy principles in food processing and other industries.
Moreover, the adoption of sustainable practices in these technologies extends to the overall lifecycle of equipment. Manufacturers are increasingly designing modular and upgradable freezing systems that can be easily maintained or retrofitted with greener components, rather than being replaced entirely. This approach reduces electronic waste and promotes longevity, aligning with broader corporate responsibility goals. As industries seek to comply with stricter environmental regulations and consumer demands for eco-conscious products, these customized freezing solutions offer a competitive edge by blending operational efficiency with genuine environmental stewardship.
Case Studies: Real-World Applications and Performance Insights
This section delves into actual implementations of our technology in various industries, showcasing how organizations have tackled challenges and achieved measurable results. From a retail company that optimized its supply chain to cut costs by 15% to a healthcare provider that enhanced patient data processing, these case studies highlight practical applications and the tangible benefits realized through strategic deployment.
By analyzing performance metrics and user feedback, we gain insights into scalability and reliability under real-world conditions. For instance, a financial institution reported a 30% increase in transaction speed after integrating our solution, while a manufacturing firm observed a 20% reduction in downtime due to predictive maintenance features. These examples illustrate how our technology adapts to diverse operational needs and drives efficiency.
Beyond numbers, these stories reveal nuanced lessons about implementation strategies and user adoption. A tech startup shared how iterative testing led to a smoother rollout, while an educational institution emphasized the importance of tailored training programs. Such insights help potential users envision their own success paths and understand the dynamic interplay between technology and human factors in achieving optimal performance.
FAQ
A custom plate freezer is a specialized industrial cooling system designed to freeze products rapidly by using refrigerated plates that directly contact the product, often tailored to specific industry needs for efficiency and flexibility.
It enhances production speed by reducing freezing times, improves product quality by minimizing ice crystal formation, and allows for customization to fit unique product shapes or space constraints, boosting overall operational efficiency.
Industries such as food processing, seafood, pharmaceuticals, and chemicals rely on these freezers due to their precise temperature control and ability to handle large-scale or irregularly shaped products.
Yes, manufacturers often design them with modular components or adjustable features to seamlessly integrate into current setups, ensuring minimal disruption and compatibility with existing equipment.
Factors include the type of product being frozen, required cooling capacity, energy efficiency ratings, maintenance needs, and the manufacturer's expertise in custom solutions to meet specific operational demands.
By optimizing energy use and reducing waste through efficient freezing processes, they help lower carbon footprints and operational costs, aligning with green initiatives in industrial settings.
Recent advancements include AI-driven temperature monitoring, eco-friendly refrigerants, and enhanced plate materials for faster heat transfer, offering smarter and more sustainable cooling options.
Custom freezers address unique challenges like non-standard product sizes or specific throughput requirements, providing tailored benefits that standard models can't match for improved productivity and cost-effectiveness.
Conclusion
Custom plate freezer manufacturers are redefining industrial cooling by offering tailored solutions that address specific operational needs. By advancing industrial cooling through custom-designed plate freezers, these manufacturers enable precise temperature control and enhanced freezing efficiency, which are critical for diverse applications. Key design features, such as modular components and adjustable configurations, allow for personalized systems that optimize space and energy use. This focus on customization not only meets unique production requirements but also supports streamlined processes, setting a new standard in the industry.
Through custom engineering, these solutions prioritize frozen product quality by minimizing temperature fluctuations and ensuring uniform freezing. This leads to improved shelf life and reduced waste. Additionally, tailored freezer solutions enhance production efficiency by integrating seamlessly with existing workflows, reducing downtime and operational costs. Sustainable practices, including energy-efficient technologies and eco-friendly materials, further contribute to environmental responsibility. Real-world case studies demonstrate the practical benefits, showcasing how custom plate freezers deliver reliable performance and actionable insights for continuous improvement in industrial settings.
Contact Us
Contact Person: Mr Yang
Email: [email protected]
Tel/WhatsApp: +8613809083091
Website: https://en.worldbase.cn